




IMA - Blister Packaging Line
or
Call +390514086204


Specifications
| Manufacturer | IMA |
| Model | C80 + A81 |
| Year | 2008 |
| Stock Number | MLTC-0002-WH |
Description
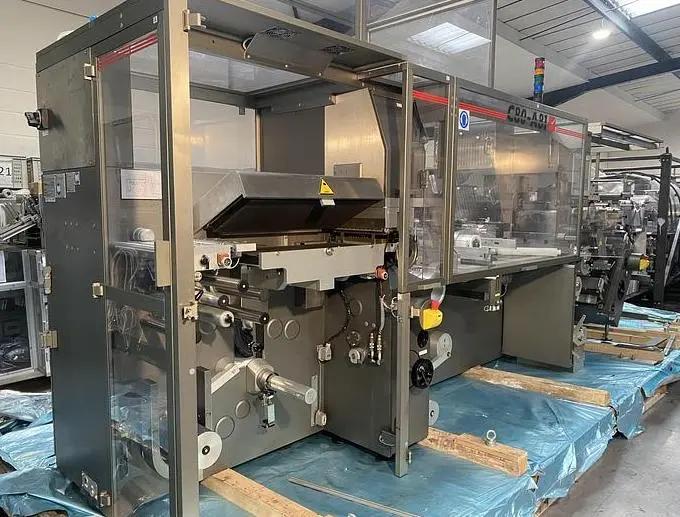
IMA BLISTER PACKAGING LINE
Year of construction: 2008
Consisting of C80 blister packing machine and A81 cartoning machine.
- Wide blister format size range
- Maximum flexibility in layout
- Fast and computer guided changeover
- Complete accessibility of the material work flow
Designed to produce blisters on two or three rows according to the size of the produced blister.
- 5441 running hours
- Easy forming materials loading thanks to the ergonomic position of the reel holder
- Automatic blister recovery magazine
PRODUCTION
- Blister dimensions: width 30-90mm, length 60-150mm, depth/height 3-12mm
- Carton dimensions: width 35-93mm, length 70-155mm, depth/height 12-90mm
- Production output: up to 400 blisters/min and up to 250 cartons/min
SET UP
- Forming station measures: 20mm x 11mm x 7mm deep (capsule)
- Pack size: 88mm x 52mm, 5 x 2 packs of 10 capsules per pack
- Carton size: 100mm x 55mm x 30mm horizontally opposed
- Trifold leaflet folder leaflet size: 118mm x 160mm before folding
PVC/PP/PET/Polymer base film with thermal forming and ALU lidding foil, twin lane. Will also run ALU/ALU with the correct tooling/format parts.
- The machine's control architecture consists of two personal computers: one runs the check and control function for the machine's functions whereas the other one runs Operator Interface function and displays alarms and archives the production setup programming parameters
- The C80/A81 is equipped with a package quality control system that is based on a series of sensors that detect any process anomalies. The defective packages are expelled into specific rejection stations
- Absolute angular transducers detect the angular position of the main kinematisms. The control logic supplies the signals necessary for the correct carrying out of all the product's processing stages
- The temperatures of the heaters are controlled by heat control units fed back by thermocouple probes
- The heat control units pilot the heating elements through static power relays